Risk assessment of oil mist: obligations, limit values and protective measures
The risk assessment for oil mist is one of the central obligations of every employer in metalworking. Even low workplace concentrations of cooling lubricant mist can lead to respiratory illnesses, skin irritation, and long-term health problems.
To systematically identify these exposure risks and derive effective protective measures, the Hazardous Substances Ordinance (GefStoffV) mandates a documented hazard analysis. For companies with CNC machines, lathes, or grinding systems, this means that without a proper assessment of oil mist exposure and the associated aerosol exposure, companies risk not only the health of their employees but also substantial fines.
What is oil mist and why does it require a hazard assessment?
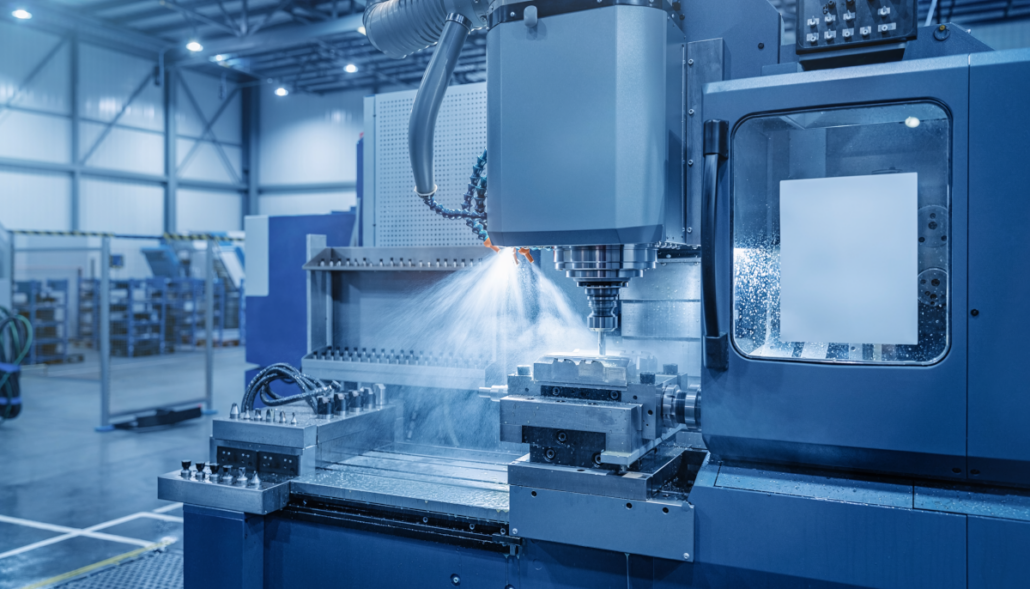
Oil mist is created by the release of fine oil droplets into the air, forming a harmful aerosol. In machining processes such as turning, milling, grinding, and drilling, the cooling lubricants and coolants used atomize into particles in the micrometer range due to high cutting speeds and injection pressures.
In addition to the visible emulsion mist, higher temperatures also produce oil fumes, which consist of even finer particles and penetrate deeper into the respiratory tract. Thermal processes intensify this effect, for example, when hot machine parts cause oil to evaporate or when minimum quantity lubrication (MQL) is used.
The invisible aerosol droplets spread through the air in the hall and settle on surfaces, machines, and electronic controls. These deposits impair air quality throughout the entire work environment and, in the case of oily residues near heat sources, can even pose a fire hazard.
Visible signs such as oily residue on walkways or cloudy indoor air indicate increased exposure. At Kaweha, our project planning experience shows that many companies underestimate the spread of oil mist: A single unventilated lathe can measurably increase the concentration throughout the entire workshop area when using flood lubrication, affecting even workstations initially classified as non-critical in the risk assessment.
The Hazardous Substances Ordinance therefore obligates employers to conduct a risk assessment before employees begin work involving exposure to oil mist. This obligation applies regardless of company size and covers all workplaces where cooling lubricants, emulsions, or cutting oils are used. Where industrial extraction and filtration systems are lacking, the concentration of oil in the air typically rises quickly above permissible levels.
What legal principles apply to the risk assessment for oil mist?
The legal basis is a combination of the Hazardous Substances Ordinance (GefStoffV), the Occupational Health and Safety Act (ArbSchG), and several Technical Rules for Hazardous Substances (TRGS). Section 6 of the GefStoffV specifies the requirements for information gathering and risk assessment: The employer must determine whether hazardous substances are generated or released during work activities and assess all resulting hazards. Sections 7 to 9 of the GefStoffV then regulate the derivation and implementation of suitable protective measures.
TRGS 402 describes the procedure for determining and assessing inhalation exposure to hazardous substances in the workplace. It specifies how workplace measurements are to be carried out and documented. Additionally, TRGS 400 defines the general framework for hazard assessment in activities involving hazardous substances.
Particularly relevant for metalworking is TRGS 611, which formulates usage restrictions and testing requirements for water-miscible cooling lubricants, for example to prevent nitrosamine formation.
The Workplace Ordinance (ArbStättV) sets additional requirements for indoor air quality and requires that harmful air pollutants be reduced to a minimum through suitable ventilation and extraction measures.
Workplace exposure limits and assessment criteria for oil mist
The limit values for cooling lubricants are complex, as TRGS 900 does not provide uniform general values for cooling lubricants. Instead, different assessment criteria apply depending on the type of substance.
Overview of the relevant limit values and assessment criteria
| KSS type | Assessment criteria | Value | fraction | source |
| Mineral oils, highly refined | Workplace exposure limit (WEL) | 5 mg/m³ | Alveolar receptive (A) | TRGS 900 |
| Water-mixed coolant | Technical assessment criteria | 10 mg/m³ | Total vapor + aerosol | DGUV Rule 109-003 |
| General dust limit value (E-fraction) | AGW | 10 mg/m³ | Inhalable (E) | TRGS 900 |
| General dust limit (A-fraction) | AGW | 1.25 mg/m³ | Alveolar receptive (A) | TRGS 900 |
| Single substance occupational exposure limit (e.g. diethanolamine) | Substance-specific occupational exposure limit (OEL) | 0.5 mg/m³ | Inhalable (E), dermally absorbed | TRGS 900 |
Important: The occupational exposure limit (OEL) of 5 mg/m³ for highly refined mineral oils refers to the respirable fraction and directly affects non-water-miscible cutting oils and grinding oil products. The value of 10 mg/m³ for water-miscible metalworking fluids (MWFs) from DGUV Regulation 109-003 is a technical guideline, not a health-based limit value.
He describes the concentration achievable according to the state of the art. The substance-specific limit values of the individual components contained in the metalworking fluids, such as emulsifiers, biocides, and corrosion inhibitors, must also be observed.
Compliance with these values can be verified using various measurement methods. Gravimetric methods collect oil mist particles on a filter and determine the mass concentration by weighing.
Optical measuring devices such as scattered light photometers record the particle size distribution in real time. Electronic particle counters complement the measurement spectrum and provide precise data on the number and size of aerosol droplets.
The German Social Accident Insurance Institution for the Wood and Metal Industries (BGHM) recommends repeating workplace measurements at regular intervals, especially after changes in the production process, after a change of the cooling lubricant or in the event of employee complaints.
At Kaweha, we know from over 30 years of project planning experience that the results of such measurements often surprise companies: In CNC machining centers with high spindle speeds and flood lubrication, the actual concentrations are regularly significantly above the technical assessment benchmark of 10 mg/m³.
Especially during grinding processes with non-water-miscible cutting oils, the combination of high thermal stress and fine droplet distribution creates aerosol concentrations that, without suitable oil mist separators and extraction and filter systems, significantly exceed the occupational exposure limit (OEL) of 5 mg/m³.
What health hazards does oil mist cause in the workplace?
Oil mist poses a serious health hazard. The fine aerosol droplets penetrate deep into the lungs via the respiratory tract and can cause chronic damage with prolonged exposure.
Among the most common consequences are respiratory illnesses such as chronic bronchitis and asthma. According to the German Social Accident Insurance (DGUV), these are caused by the oil droplets penetrating deep into the lungs and their chemical additives such as emulsifiers and preservatives.
The International Agency for Research on Cancer (IARC) classifies untreated and mildly treated mineral oils as carcinogenic to humans (Group 1). This classification is primarily based on the proven association with skin cancer following occupational exposure.
Highly refined mineral oils, such as those predominantly used in modern metalworking fluid formulations, fall into IARC Group 3 (not classifiable as to cancer risk). The quality of the base oil used therefore plays a crucial role in risk assessment.
Besides affecting the respiratory system, oil mist also attacks the skin. Repeated contact with oil-containing aerosols can lead to contact dermatitis and oil acne. Additionally, the chemical components in oil mist cause acute symptoms such as headaches, nausea, and dizziness, especially in poorly ventilated work areas.
A particularly insidious long-term consequence is so-called lipid pneumonia, in which inhaled oil particles accumulate in the lungs and trigger chronic inflammation.
In addition, there is an aspect that is often neglected in risk assessments: oil mist deposits on hall floors and machine surfaces significantly increase the risk of accidents due to slipping hazards.
At the same time, the deposits attack electronic controls and sensitive sensors, leading to machine failures and increased maintenance. All these health and safety risks underscore why a thorough hazard assessment and effective technical protective measures, such as the extraction of oil and emulsion mist directly at the source, are essential.
How is a hazard assessment for oil mist carried out?
The risk assessment for oil mist follows a structured process described in TRGS 400 and TRGS 402. The aim is to determine the actual exposure of employees and to define appropriate protective measures.
The first step involves identifying all workplaces where oil mist, emulsion mist, or oil fumes may occur. This includes CNC machining centers, grinding machines, lathes, and all other machine tools that use cooling lubricants or coolants.
For each workplace, the type of cooling lubricant used (water-miscible or non-water-miscible), the quantities consumed, and the spatial conditions are recorded.
A common mistake in practice: The assessment is limited to the immediate vicinity of the machine, without considering the actual spread of aerosols throughout the hall. Open machine housings, a lack of enclosures, and thermal effects from warm workpieces can cause the oil mist to spread far beyond the actual machining area.
The second step involves determining exposure. TRGS 402 distinguishes between an estimation without measurement and a measurement-based determination. Estimation utilizes existing data such as safety data sheets, empirical values, and industry comparisons.
Measurement-based determination provides more precise results and is particularly necessary when estimation does not allow for a clear conclusion. Especially in mixed machinery where water-miscible and non-water-miscible cooling media are used simultaneously, measurement-based determination is recommended, as the aerosol composition varies considerably depending on the type of cooling media and different limit values apply.
In the third step, the results are evaluated and compared with the respective assessment criteria. If the measured concentration exceeds the applicable limits, protective measures must be taken immediately.
The entire assessment must be documented and updated regularly. The BGHM recommends an update cycle of at least three years, and more frequently in the event of significant changes to the production process.
What protective measures are derived from the risk assessment?
The selection of protective measures follows the STOP principle (Substitution, Technical, Organisational, Personal), which establishes a clear hierarchy.
Substitution is the first priority: Can the coolant used be replaced by a less hazardous alternative? In some applications, switching to minimum quantity lubrication or dry machining can drastically reduce the formation of oil mist and emulsion mist.
In practice, however, substitution reaches its limits in many manufacturing processes: grinding and honing processes, for example, still require an intensive supply of coolant to achieve the required surface finishes and tolerances. In such cases, technical measures become paramount.
Technical measures form the core of effective oil mist reduction. Extraction systems located near machines capture the aerosols directly at the source before they can spread into the hall air.
Modern oil mist separators operate with multi-stage filtration: First, coarse particles and droplets are retained in the pre-separation stage by mechanical stainless steel mesh filters. These filters utilize the coalescence principle: The fine oil droplets combine on the filter fibers to form larger droplets, which are then collected and conveyed into collection containers.
The main separation of oil mist and emulsion mist then takes place, and a post-filtration process using HEPA filters (high-efficiency particulate air filters) removes the remaining particles from the air. Mechanical filtration has proven to be the more efficient option compared to electrostatic separators in recent years, both in terms of separation efficiency and filter lifespan in continuous operation on production lines.
High-performance systems such as the Oilmaster OM Reverse from Kaweha achieve separation efficiencies of up to 99.95% with a residual value content of the purified air of less than 5 mg/m³.
When selecting the right extraction solution, the results of the risk assessment are directly incorporated into the system design. The type and concentration of the cooling lubricant, the number of machines to be covered, the required volume flow, and the spatial conditions determine whether a single-station solution or a central extraction system is the right choice.
At Kaweha, we rely on the specific measurement data from the risk assessment for dimensioning, as general estimates often lead to undersized systems and thus to continued excessive concentrations in the workplace.
The determined volume flow rate is the central design parameter: Depending on the enclosure, a CNC machining center with a closed machine housing and flood lubrication requires a measured volume flow rate that is far higher than what many companies initially assume.
For individual machines or smaller groups of machines, a mobile single-station solution such as the Oilmaster Mini R ST/M with a volume flow of 600 to 1,500 m³/h is suitable.
For four or more machines in one hall area, a central extraction system with shared piping is usually more economical: The stationary Oilmaster OM R covers volume flows from 1,500 to 100,000 m³/h and is designed for 24/7 continuous operation on production lines.
The advantages of a correctly designed extraction system are considerable: clean air throughout the entire work area, compliance with health and safety regulations, reduced wear and tear on equipment and electronic controls, and a longer service life for production machines.
An often underestimated additional benefit is the recovery of cooling lubricant: The separated oil droplets are collected in reservoirs and can be returned to the cooling lubricant circuit. For companies with high oil consumption, this allows the extraction system to pay for itself more quickly.
Organizational measures complement the technical solution. These include regular maintenance and care of the cooling lubricants according to TRGS 611, training of employees in the safe handling of cooling lubricant emissions, and adherence to maintenance intervals for the extraction system.
Modular filter configurations, such as those used in industrial extraction systems, can be adapted to changing production conditions and expanded with activated carbon filters to eliminate aromatics and odors.
The maintenance of the cooling lubricant itself also has a direct impact on emissions: Over-aged or microbially contaminated emulsions produce significantly more aerosol and odor than freshly prepared and correctly monitored cooling lubricants.
Regular monitoring of concentration, pH value and germ load according to TRGS 611 is therefore necessary not only from a hygienic point of view, but also from an extraction point of view, as higher aerosol loads shorten filter service life and increase the maintenance effort of the extraction system.
Personal protective equipment (PPE) such as respirators with A2P3 filters is only used if the aforementioned measures cannot sufficiently reduce exposure.
According to the basic principle of TRGS 500, technical measures such as oil mist separators and extraction systems take precedence over organizational measures and personal protective equipment.
Documentation requirements and inspection deadlines
The results of the risk assessment must be documented in writing. This documentation includes the identified hazards, the defined protective measures, the results of the effectiveness review, and the date of the next review.
For workplaces with oil mist exposure, the BGHM (German Social Accident Insurance Institution for the Wood and Metal Industries) recommends updating the risk assessment at least every three years. The Hazardous Substances Ordinance (GefStoffV) itself stipulates regular review and needs-based updates in Section 6, Paragraph 8, without specifying a fixed interval.
Early inspection is required in any case when changing the cooling lubricant, when changing the machine equipment or the production process, in the event of complaints or health problems of employees, after work accidents related to oil mist exposure and in the event of new scientific findings or changed limit values.
The documentation must be available for inspection by the responsible supervisory authority at all times. Evidence of workplace measurements, regular maintenance of installed extraction and filter systems, and training materials are also part of the complete documentation.
One point that is often overlooked in practice: Maintenance records for the extraction system are an integral part of the risk assessment. A dirty or saturated filter, a leaking duct, or a worn-out fan can drastically reduce extraction performance, meaning that the protective effect assumed in the assessment is no longer guaranteed.
Kaweha therefore recommends integrating the maintenance intervals of the extraction system into the risk assessment cycle. A maintenance contract provides complete documentation of your system's functionality and simultaneously fulfills your reporting obligations to the regulatory authority.
KAWEHA: Your partner for clean air in the workplace
The results of the hazard assessment form the basis for designing an effective extraction solution. As a manufacturer of industrial extraction and air filtration systems since 1991, Kaweha develops customized systems at its Lohfelden site near Kassel, designed based on your specific measurement data and production conditions.
From consulting, planning and assembly to commissioning and ongoing service with maintenance contracts, we accompany you throughout the entire life cycle of your extraction system.
Whether a single-station solution with the Oilmaster Mini R ST/M on a CNC machine or a central extraction system with the Oilmaster OM R for an entire production hall, whether ATEX-compliant systems for explosion-hazardous areas or special constructions with individually manufactured capture elements: Kaweha designs each system based on the actual exposure data so that you can permanently comply with the limit values and create a healthy working environment for your employees.
Frequently asked questions (FAQ)
Who is responsible for the risk assessment in the case of oil mist?
The employer is responsible for conducting and documenting the risk assessment. They can delegate this task to qualified personnel, such as the occupational safety specialist or the company physician. However, the ultimate responsibility remains with the employer.
How often does the risk assessment need to be updated?
The Hazardous Substances Ordinance (GefStoffV) requires regular review and updates as needed. The German Social Accident Insurance Institution for the Wood and Metal Industries (BGHM) recommends a cycle of at least three years as a guideline. In the event of significant changes to the production process, a change of cooling lubricant, or if employees experience health problems, the assessment must be reviewed immediately.
What are the limit values for oil mist in the workplace?
For highly refined mineral oils (non-water-miscible cutting oils), an occupational exposure limit (OEL) of 5 mg/m³ applies to the respirable fraction according to TRGS 900. For water-miscible metalworking fluids (MWFs), DGUV Regulation 109-003 defines a technical assessment criterion of 10 mg/m³ (sum of vapor and aerosol). In addition, the substance-specific limit values of the individual components must be observed.
What happens if the limit values are exceeded?
If the assessment criteria are exceeded, protective measures must be taken immediately. Until technical measures such as extraction systems are effectively implemented, suitable personal protective equipment must be provided to employees. Repeated violations may result in fines.
What role do extraction systems play in risk assessment?
Extraction systems are generally the most effective technical measure for reducing oil mist exposure. The results of the hazard assessment determine the requirements for the extraction system, such as the required volume flow, the separation efficiency, and the type of filtration.
The measurement data is directly incorporated into the system design: This is the only way to ensure that the extraction capacity is sufficient for the actual emissions during operation. As a manufacturer of industrial extraction and air filtration systems, Kaweha offers customized solutions designed based on the specific measurement results.
Do small businesses also have to carry out a risk assessment?
Yes, the obligation to conduct a risk assessment applies regardless of company size. Even small craft businesses or workshops that work with cooling lubricants must assess and document their employees' exposure. Aerosol concentrations rise particularly quickly in small production areas with limited space, which is why a mobile, individual workstation solution is often the most economical measure.
February 24, 2026
